Flatbed die cutting presses a flat tool down onto the material in a cyclic stroke. Rotary die cutting runs a cylindrical tool against the material continuously. The mechanical difference sounds small and turns out to decide almost everything: achievable speed, tooling cost, substrate range and how much time you lose on every job change.
GB standard reference
- Standard
- GB/T 1299 (alloy tool steel) · GB/T 1220 (stainless)
- GB grades in this article
- W6Mo5Cr4V2 · Cr12Mo1V1 · Cr8Mo2SiV
- Also sold as
- M2 / SKH51 · SKD11 / D2 · DC53
- Hardness range
- HRC 58-63
1. The Mechanical Difference and Why It Matters
A flatbed machine generates cutting force with a toggle or knuckle mechanism that closes a platen, so force is applied to the whole sheet at once. A rotary machine applies force progressively along a line of contact between two cylinders. Each approach has a direct consequence.
| Rotary | Flatbed | |
|---|---|---|
| Material feed | Continuous roll (web) | Sheets or roll (with a feeder) |
| Cutting action | Continuous, cylinder against anvil | Cyclic stroke, platen closes |
| Typical speed | Hundreds of metres per minute | Sheets per hour, limited by stroke cycle |
| Cut depth control | Set once by the die/anvil gap | Re-established per make-ready |
| Tooling first cost | High — a machined cylinder | Lower — a flat cutting plate |
| Tool change | Slow, whole cylinder | Fast, plate swaps in the chase |
| Thick and dense substrates | Limited by board caliper | Better — the press opens wide |
| Functions in one pass | Yes — print, perforate, laminate, slit | Possible but limited by station count |
2. Speed and Precision
Rotary's advantage is continuous motion. Because the tool never stops and never lifts, throughput is several times that of a flatbed machine on the same job, and cut depth is set once instead of re-established at every make-ready. That stability is why rotary tooling generally holds a tighter cut-depth window — which is the whole basis of a reliable kiss-cut.
Flatbed's advantage is force and openness. The press can be opened wide, so it handles thicker and denser materials than a rotary station tolerates, and it accommodates a much wider range of substrates, including sheets that a web-fed machine cannot take at all.
3. Tooling Cost and Changeover
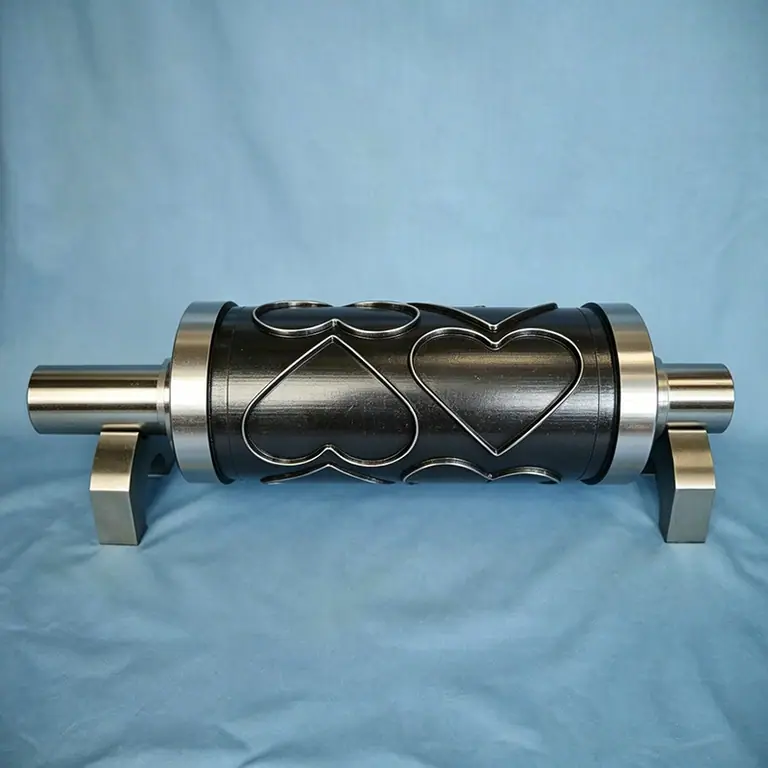
This is where the decision usually gets made. A rotary die is a machined, hardened and balanced cylinder: a substantial piece of work with a lead time measured in weeks. A flatbed cutting plate costs far less and is quicker to produce, and changing it is a matter of swapping the plate in the chase rather than pulling a cylinder off the press.
For frequently changing batches, that difference dominates. For a job that runs continuously for months, the rotary tool's higher cost is amortised into irrelevance while its speed advantage compounds every shift.
For short and mid-run roll-fed work there is a middle path: an oscillating (semi-rotary) tool, or a segmented die whose inserts can be swapped cheaply when the design changes. Both approach flatbed tooling economics while keeping the web continuous.
4. Substrate Range
| Substrate | Rotary | Flatbed | Note |
|---|---|---|---|
| Pressure-sensitive label stock | Excellent | Rare in production | Rotary kiss-cut is the standard |
| Folding carton board | Very good | Very good | Either; volume decides |
| Corrugated board | Good, as segmented tooling | Excellent | Flatbed handles heavier calipers more easily |
| Thin films and foils | Excellent | Limited | Web handling favours rotary |
| Nonwovens and foams | Good | Good | Both used |
| Thick or dense sheet material | Limited | Best | Press opening and force favour flatbed |
5. Make-Ready and Downtime
Make-ready is the hidden cost in any converting decision. A rotary station needs the die and anvil gap established, register confirmed and the pressure recorded; once done, it tends to stay put for the whole run. A flatbed station needs the plate packed and pressure distributed evenly across the platen, which takes time at every job change and is where most variation between operators creeps in.
So the comparison is not simply fast machine versus slow machine. It is a long make-ready amortised over a long run versus a short make-ready repeated at every changeover. Quantify your changeover frequency before choosing, because that number usually decides more than the headline speed difference.
6. The Decision Matrix
| If your situation is… | Choose | Because |
|---|---|---|
| High volume, roll-fed, one design for months | Rotary | Speed and cut-depth stability compound over the run |
| Frequent design changes, shorter batches | Flatbed (or segmented inserts on a rotary die) | Tooling cost and changeover time dominate |
| Thick or dense sheet material | Flatbed | Press can be opened wide; force is applied to the whole sheet |
| Printed labels with tight register to the die cut | Rotary | In-line register and multiple functions in one pass |
| Corrugated board above ~2 mm caliper | Flatbed, or segmented rotary on the corrugator | Thicker board favours flatbed; high volume justifies segments |
| Thin films and foils | Rotary | Continuous web handling, no sheet feeding |
| Prototype and first-article validation | Flatbed | Cheapest tooling to make and modify |
Rotary is not the better process; it is the better process for continuous, high-volume, roll-fed work. Flatbed is not the older process; it is the better process when the tool has to change often or the material is thick.
Rotary vs flatbed: frequently asked questions
It generally holds a tighter and more consistent cut-depth window, because the die-to-anvil gap is established once and the tool never lifts. Flatbed can achieve excellent accuracy too, but pressure has to be distributed evenly across the platen at every make-ready, which introduces more run-to-run variation.
We manufacture rotary tooling and supply die-grade hardened bar for flatbed cutting rules, so we have no incentive to steer you one way. Send us the substrate, the run length and the caliper and we will tell you which process we would choose.